

A bill of materials (BOM) in supply chain management is the list that tells purchasing what to buy, how much of it and by when, for every product a factory makes. On the shop floor, it reads as a parts list, but once it goes out into the supply chain, it turns into purchase orders, supplier lead times and delivery dates, and that is where most of its effect ends up being felt.
This article covers what the BOM does on that supply chain side, and the ways it tends to go wrong.
Where a BOM Sits in the Supply Chain
Building and version-controlling a BOM inside an ERP is covered in Synergix’s guide to bill of materials management. Once it is built, the BOM starts driving decisions that involve suppliers, and it does that in four main ways.
Turning a sales order into purchase demand
A sales order for 200 units means very little to a purchasing team until it has been multiplied out through the BOM. Each component quantity gets multiplied by 200, the stock already on hand is taken off, and whatever is left over is what has to be bought.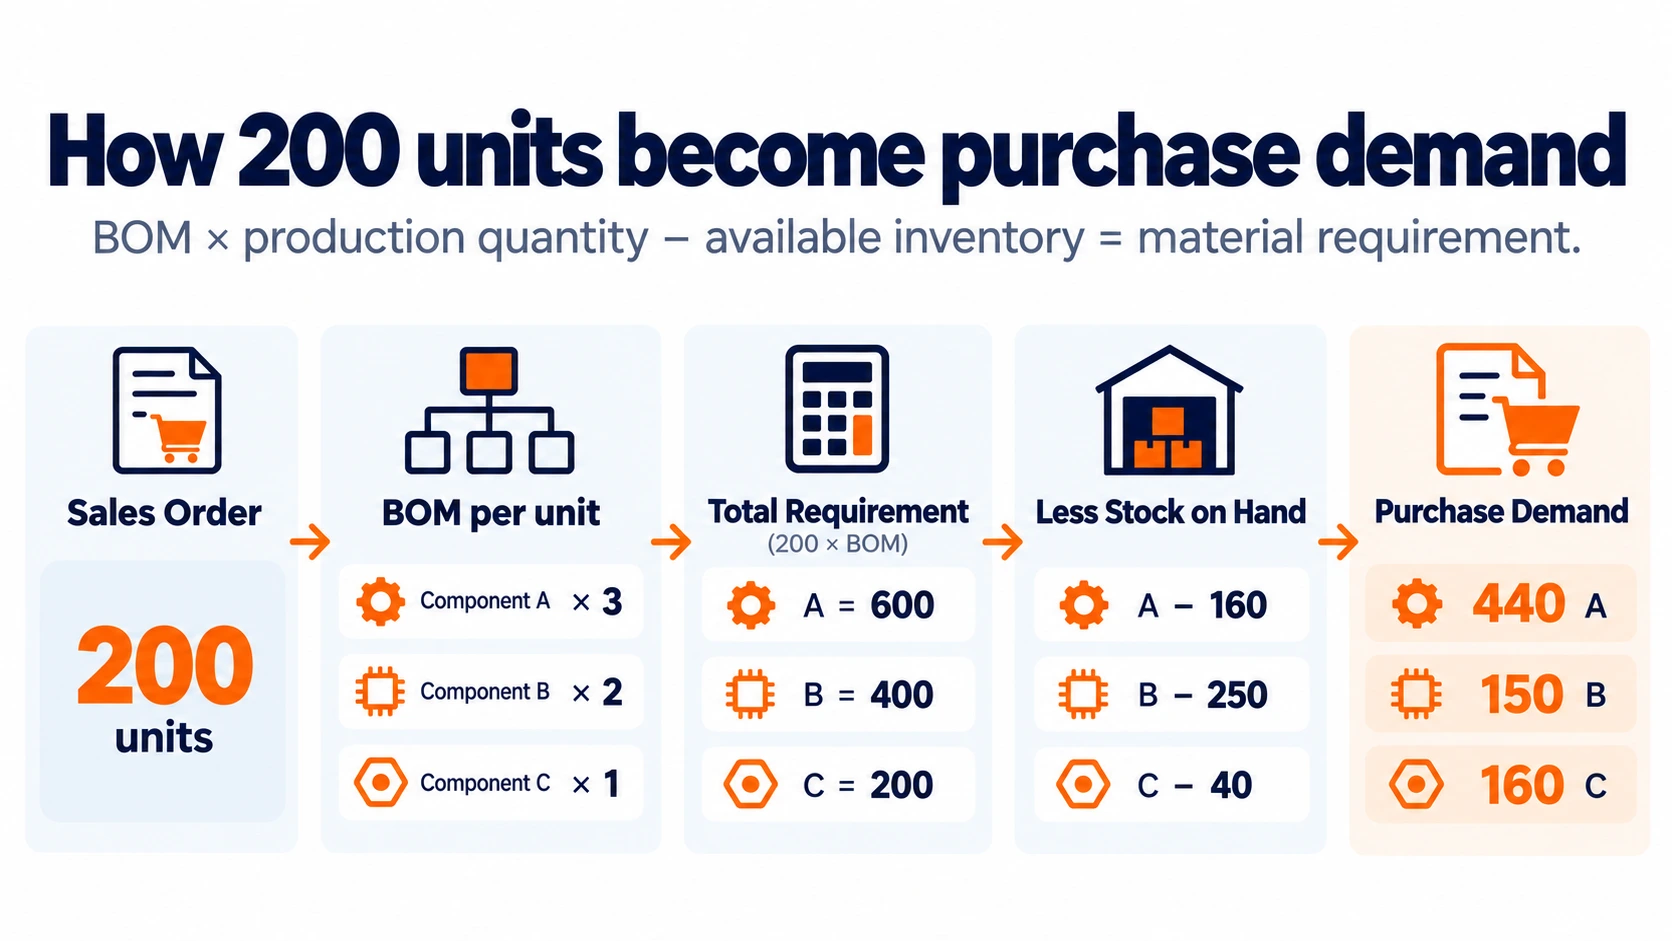 That calculation is what material requirements planning does. In Synergix ERP, production management reads the BOM structure, the production schedule and current stock together, and the requirement it produces is what becomes a purchase requisition or a purchase order.
With a multi-level BOM, the same thing happens at each level, so a sub-assembly made in-house creates its own demand for the parts underneath it.
Timing purchases against supplier lead times
Knowing how much to buy is only half of it. The other half is knowing when, and that comes down to supplier lead times. A component with a six-week lead time has to be ordered six weeks before the production stage that uses it, and not at the point where somebody notices the bin is empty.
MRP works this out from the planned start date of each job and the lead time recorded against each item, so purchasing is timed to production and not left to react to it. Supply chain management in the same system then carries that timing through to the supplier side.
Engineering BOM vs manufacturing BOM
Engineering designs a product using an engineering BOM. Production needs a manufacturing BOM, and that one also has to cover how the product is put together. Purchasing buys from whichever of the two it is handed.
| Engineering BOM (EBOM) | Manufacturing BOM (MBOM) | |
|---|---|---|
| Question it answers | What is the product made of? | How does the product get built? |
| Owned by | Engineering | Production |
| Covers | Designed components and assemblies | EBOM content plus fasteners, consumables, packaging and assembly sequence |
| Drives | Design intent, cost estimates | Work orders, MRP, purchase orders |
Purchasing should be working from the manufacturing BOM. When a design changes, both have to move together, and the supply chain only stays lined up for as long as they do.
Tracing a part back to its source
When a batch fails, what everyone wants to know is which supplier lot it came from and what else that lot went into. The BOM is the thing connecting a finished product back through its components to the purchase orders and quality records behind them.
Fong Lee Metal Industries, a Singapore precision engineering firm, describes this in its own account of using Synergix. Purchase orders and quality records can now be searched and viewed easily, and its manufacturing execution system shares information with the ERP through an API right across the process.
Compliance adds to the need. Singapore’s National Environment Agency restricts six hazardous substances in a defined list of electrical and electronic products, and firms selling into the EU face broader rules that reach down to parts and components. In both cases, proving a product complies means knowing exactly which components went into it.
The Supply Chain Risks of a Weak BOM
A manufacturer running a few dozen products is maintaining a few dozen bills of material, and the errors in them fail in fairly predictable ways.
One wrong quantity, multiplied
A BOM error does not stay small. If a quantity is entered as 4 where it should be 3, every work order built from that BOM over-orders by a third, and on a multi-level BOM the mistake carries down into every sub-assembly underneath as well. Unit of measure errors behave the same way; for example, a part bought in boxes of 100 but recorded per piece.
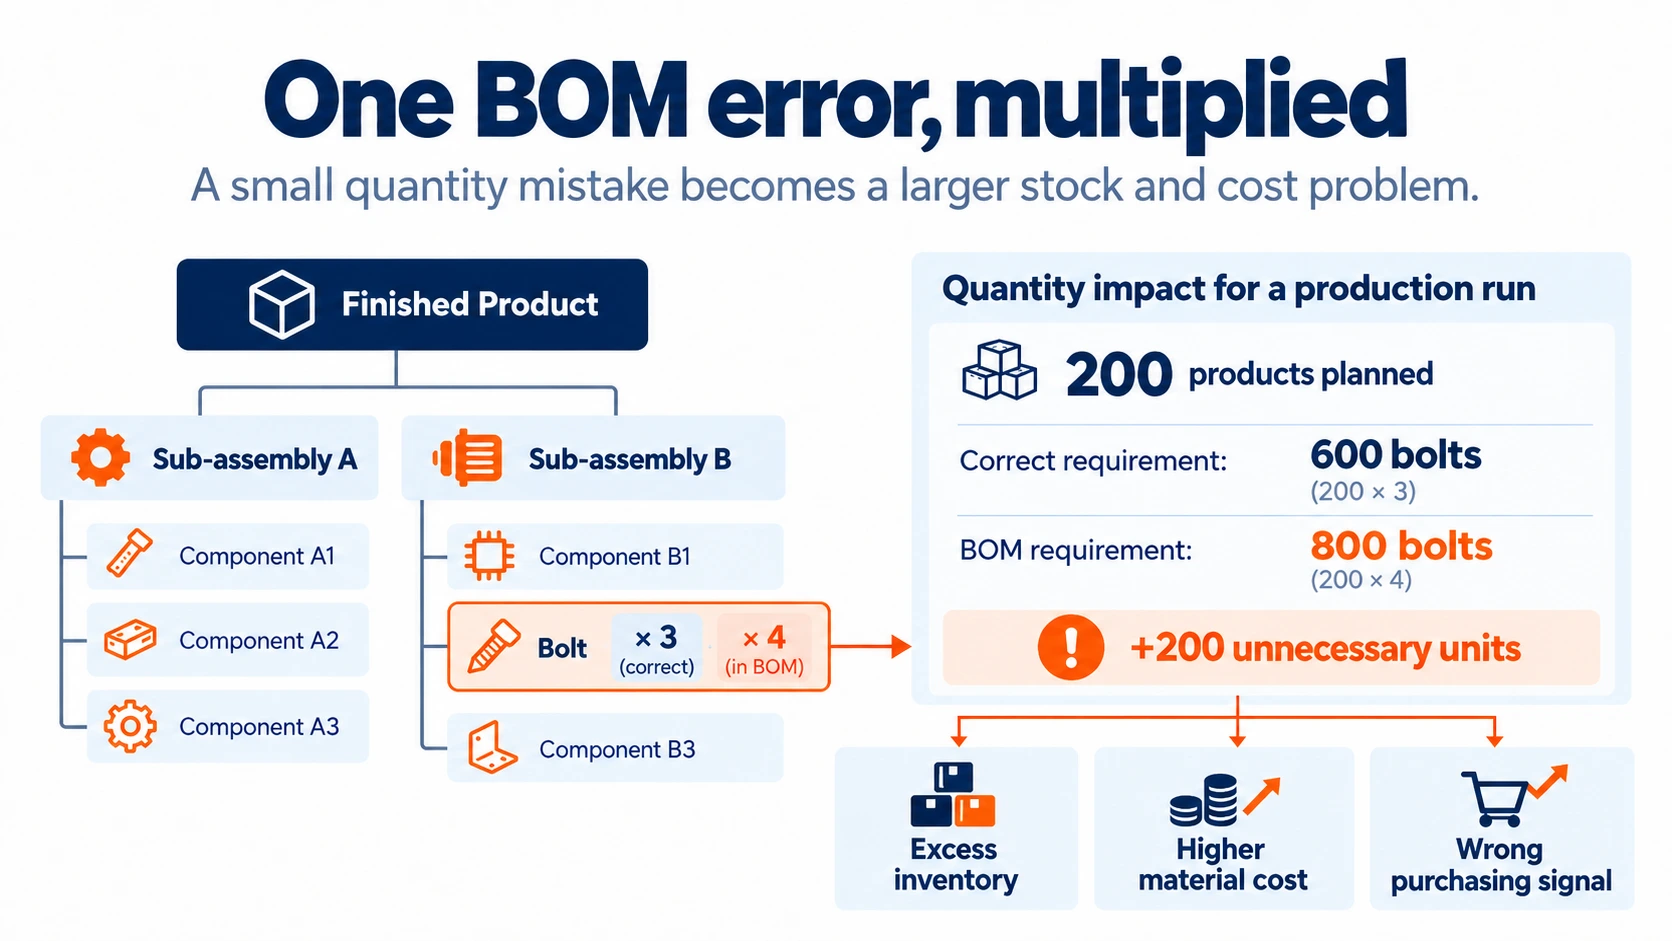 The cost then turns up in two places together: surplus stock of the part that was over-ordered, and a direct material cost on every finished product that is higher than it should be.
The component that costs a few cents
The shortages that hurt most are often of the cheapest parts. In late October 2025, a dispute over the chipmaker Nexperia cut supply of basic power control chips that cost only a few cents to buy and sit inside the electronic control units used across almost every vehicle. Honda halted production at its Celaya plant in Mexico, having already begun cutting output in the United States and Canada days earlier.
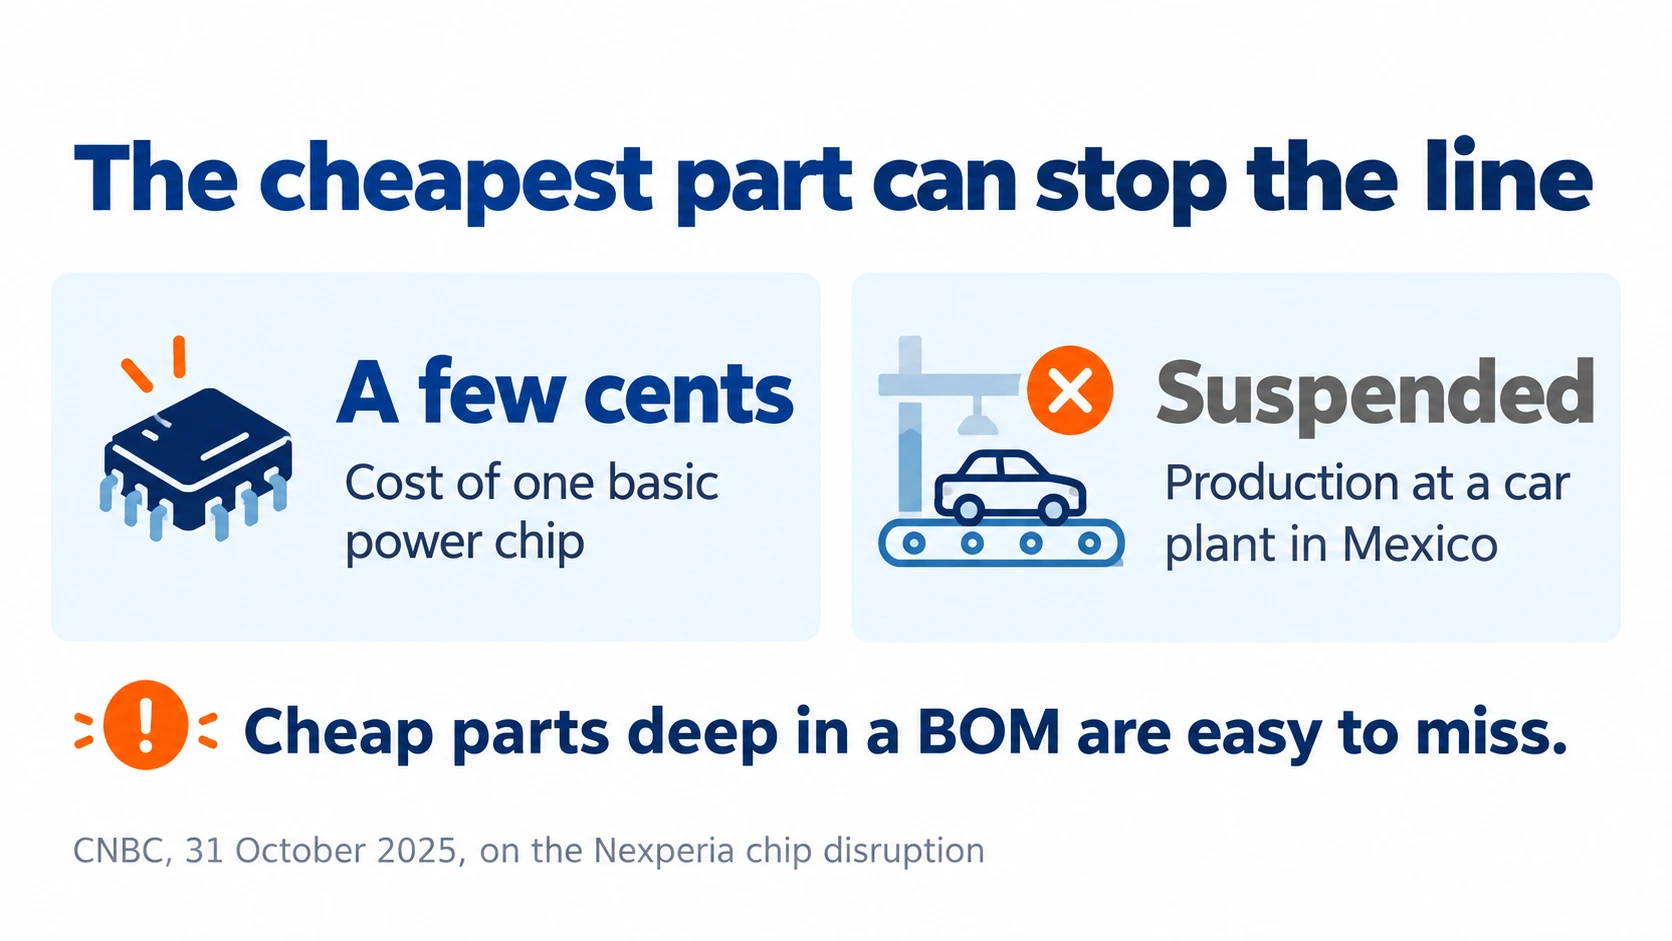 These chips mostly reach car makers inside parts that their suppliers build, so the dependency sits several levels down a multi-level BOM instead of on the top level where people tend to look. A component that never appears on the first page of a BOM can still stop the line, and a BOM recording the approved supplier for each item is what shows where those single points of failure actually are.
When engineering and production drift apart
If engineering updates a design and the manufacturing BOM does not get updated with it, purchasing carries on buying the old part. The wrong parts arrive, production cannot use them, and the right ones were never ordered in the first place.
Parts that go obsolete
Components get discontinued. If the BOM does not record that, MRP keeps creating demand for something no supplier sells anymore, and the shortage only shows itself when an order fails. Filling the gap by buying discontinued parts on the open market also brings a higher chance of receiving counterfeit or unverified components.
What a parts list leaves out
A BOM lists materials. Machine time, specialist tooling and skilled labour are often missing from it, which means material can be fully available while the job still cannot run. In Synergix, process routing is set up alongside the BOM to cover the work centres and resources that each operation needs.
A Sign the BOM is Already Wrong
Most production systems allow materials to be issued that are not listed in the BOM, since real production does not always follow the plan. Synergix’s stock issue function supports this kind of ad-hoc issuance so that work can carry on.
What is useful is what the frequency of it says. If the same item keeps being issued outside the BOM for the same product, then the BOM is missing something, and every purchase calculated from it is short by that amount. Reviewing ad-hoc issues by product and by item is a fairly direct way to find which BOMs need correcting, and it uses data the system is already recording anyway.