

Discrete manufacturing builds countable items from parts. Process manufacturing turns raw materials into bulk output using a formula. Batch manufacturing is neither of those: it describes how production is scheduled, and it happens inside discrete and process plants alike.
That distinction matters when you are choosing a system. A plant that counts units needs a bill of materials and routings; a plant that mixes to a recipe needs formulas and yield tracking; both need lot traceability if they run in batches. Our manufacturing ERP solution covers the discrete and batch side of this.
Discrete Manufacturing: Products That Can Be Counted
Discrete manufacturing produces separate items that can be counted, and often given a serial number, by putting together parts and components. A machine, a circuit board and a precision bracket are all discrete products.
Production in a discrete plant runs on two documents:
- The bill of materials says what goes into the product, and the routing says which operations it passes through and on which work centres. The same principles apply at both ends of the range, from a line turning out thousands of identical fasteners to a workshop building one machine to a customer’s specification.
- The engineer-to-order is common among Singapore manufacturers. One of our customers – Tungray Singapore – keeps all project data on the inventory BOM page in Synergix, so when a new order arrives with similar or identical requirements, the historical details are already there to work from. The firm also records costs at each phase, from procurement through fabrication to delivery, and gets a cost analysis once the project is finished.
Discrete work makes up a large part of manufacturing in Singapore. Electronics and precision engineering, two of the main clusters in EDB’s monthly manufacturing figures, consist largely of assembled, countable products.
Process Manufacturing: Products Made from a Formula
Process manufacturing turns raw materials into something new by mixing, blending, heating or reacting them according to a formula or recipe. Paint, cooking oil, shampoo and medicines are all process products.
Two things set it apart from discrete work: The instruction document is a formula rather than a parts list, and the same inputs do not always give the same output.
Some process plants run continuously for days or weeks at a time, as refineries do. Others work in separate batches, which is where the overlap with batch manufacturing comes in.
In Singapore, the chemicals cluster on Jurong Island and the pharmaceutical side of biomedical manufacturing are the clearest examples of process production.
Batch Manufacturing: A Scheduling Method Found in Both
Batch manufacturing makes a set quantity of identical items together, as one batch or lot, through a series of steps.
Each batch carries a lot number. When a quality problem surfaces, that number traces which raw materials went into the batch and which customers received it, so a recall covers the affected lot instead of everything made that month.
Singapore’s own figures show how much batch-driven production can move the numbers. EDB reports manufacturing output twice every month, once including biomedical manufacturing and once leaving it out, because biomedical is volatile enough to distort the headline figure on its own.
In December 2025, biomedical output fell 38.8% year on year, pulled down by a 69.7% drop in pharmaceutical production, which EDB attributed to a different mix of active pharmaceutical ingredients being produced compared with a year earlier. In a sector making high-value products in large separate runs, what gets produced in a given month, and when a run lands, swings the monthly figure by that much.
Why Setup Time Decides the Batch Size
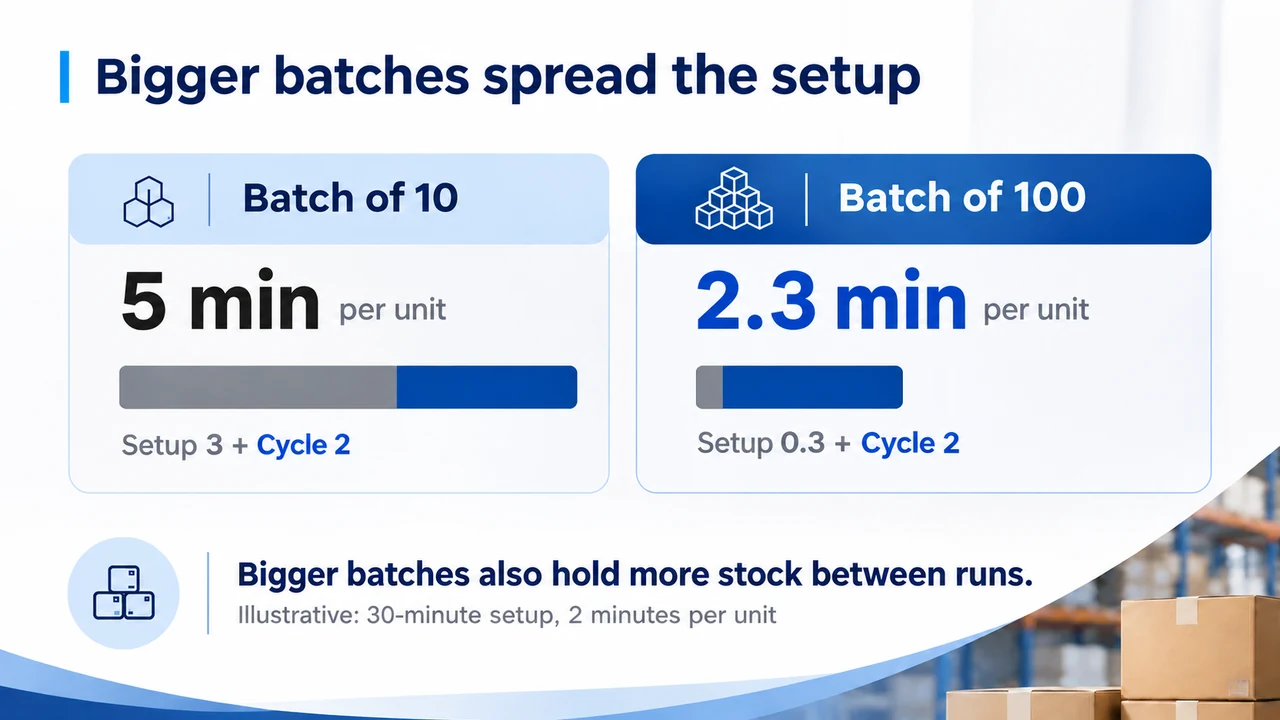
Each batch carries a fixed changeover cost: the time spent cleaning, resetting or retooling before production can start. That time stays the same whatever the batch size, so it spreads across however many units are in the batch.
With a setup of 30 minutes and a cycle time of 2 minutes per unit:
| Setup per unit | Total time per unit | |
|---|---|---|
| 10 units | 3.0 minutes | 5.0 minutes |
| 100 units | 0.3 minutes | 2.3 minutes |
Larger batches bring the cost per unit down, but they also leave more stock sitting between runs. Planners usually settle on a batch size somewhere in between.
In Synergix ERP, process routing holds setup time and cycle time as two separate figures for each operation, so planners can work the trade-off out before committing to a batch size.
Discrete vs Process Manufacturing: Side by Side
| Discrete manufacturing | Process manufacturing | |
|---|---|---|
| Output form | Countable units, often serialised | Bulk goods measured by weight or volume |
| Product definition | Bill of materials and routing | Formula or recipe |
| Yield consistency | Fixed output from fixed inputs | Yield varies between runs |
| Unit of a batch | A production run of identical parts before changeover | One mix or lot before the vessel is cleaned |
| Singapore clusters | Electronics, precision engineering, machinery | Chemicals, pharmaceuticals, food |
Where Costing Breaks in Each Type
The production type a plant runs decides where its margin leaks, and the two types leak in different places.
Discrete: the standard holds, so variance is visible
A discrete plant works from a fixed bill of materials. If the BOM says 1.2kg of steel per bracket and a run of 500 consumes 675kg instead of 600kg, the extra 75kg is scrap or rework, and it shows up as a variance against a known standard. The number to explain is obvious because the expected figure never moves.
What gets missed here is usually labour and machine time rather than material. If operators record time against a shift instead of against a work order, material cost is accurate and conversion cost is an estimate, which makes the job look cheaper than it was.
Process: the yield moves, so the standard is the problem
A process plant has no fixed output. A 200-litre formula might yield 192 litres after evaporation, residue left in the vessel and the sample pulled for QC. Nothing went wrong, and that is the point. If the system costs the batch at the theoretical 200 litres, every batch is undercosted by 4%, quietly and consistently, and no variance report flags it because the system was never told to expect anything else.
Process costing has to work from actual yield, batch by batch, with the theoretical figure kept alongside it for comparison. Over a year, a 4% gap on every run is the difference between a product line that looks profitable and one that is.
Batch: the setup cost has to land on the batch, not the unit
Changeover time belongs to the batch, not to the units inside it. A system that applies a flat overhead per unit will cost a run of 10 and a run of 100 at the same rate per unit, when the real figures are 5 minutes and 2.3 minutes.
The consequence is a pricing error rather than a reporting one. Short runs and urgent one-off orders look as profitable as full batches, so they get quoted at the same margin, and the plant absorbs the difference without seeing it. Any plant that takes frequent small orders should check how its system treats setup before it trusts a job costing report.
What to Check in a System for Each Type
Discrete production
- Bill of materials with several levels of sub-assembly and a record of who changed what and when
- A routing per product, listing operations and the work centre each runs on
- Setup time and cycle time held as separate figures for each operation
- Work orders that track progress stage by stage
- Serial or batch numbers where the product or the customer requires them
- Labour and machine time booked to the work order
Process production
- A formula holding proportions rather than fixed quantities
- Actual yield recorded per batch and compared against theoretical
- Unit of measure conversion between how material is bought, stored and consumed
- By-products and co-products costed
- Cost per litre or per kilogramme calculated from actual output
Batch running, in either type
- Lot numbering applied automatically at the point of production
- Traceability in both directions: from raw material lot to customer and vice versa
- Changeover time captured separately
- Quality hold at batch level
- Shelf life and expiry on perishable items with first-expiry-first-out picking
- Work in progress visible between runs
In Synergix ERP, the production management module is built around multi-level BOMs, routings and work orders, including batch runs within discrete production, and it keeps a history of BOM changes. The material calculation behind it is covered in our comparison of ERP vs MRP systems.
Recipe-based batch production in food works differently. The Synergix F&B solution records each recipe with its ingredients, overheads and the cooking time for each stage, works out how much of each ingredient the day’s portions need, compares estimated consumption with actual, and tracks batch and lot numbers for perishable items.
Plants running continuous process lines, such as refineries, or regulated pharmaceutical production with formal batch records, usually work with specialised process systems built for that environment.
Work out Which Type Your Plant Runs on
Most plants are clearer about this than their systems are. If your BOM structure is fighting a recipe, or batch and lot numbers are tracked outside the system, the mismatch usually shows up first in costing.
Tell us how your production runs and we will show you which parts of Synergix fit it, and which parts you would not need.